Aug.31,2026
Choosing the right resin for an insert-molded electrical component is not simply a matter of comparing tensile strength or material price. The polymer must protect metal inserts, maintain insulation, resist heat and chemicals, fill thin sections, and remain stable through repeated electrical and thermal cycles. For companies planning Insert Overmolding Services, the most useful comparison is the one that connects material data with actual component performance.
This guide compares PA66, PBT, and LCP from the perspective of purchasing teams, product engineers, and manufacturing managers. It focuses on dimensional stability, moisture behavior, electrical reliability, battery life impact, processing risk, total cost, and the types of components each material is best suited for.
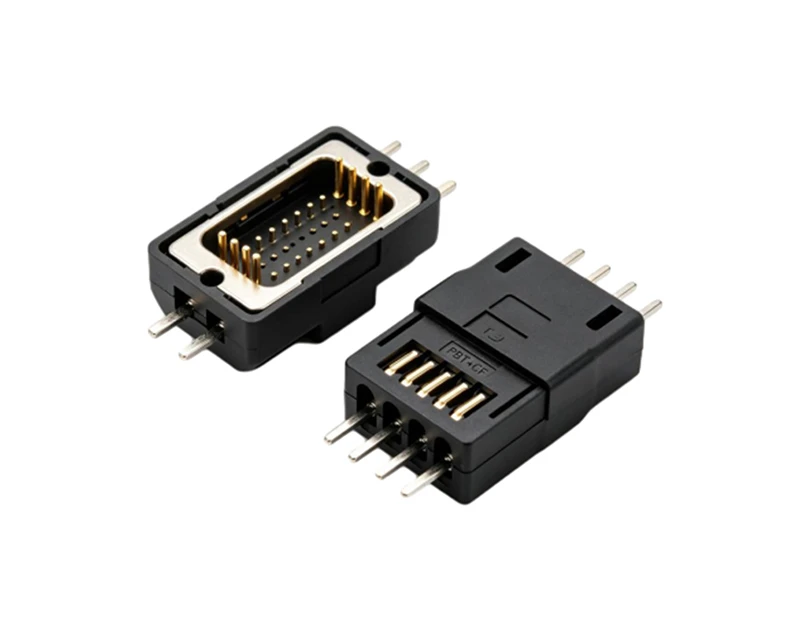
Searchers comparing PA66, PBT, and LCP usually want to reduce several risks at the same time. A material that looks inexpensive on a datasheet can create higher costs through moisture conditioning, rejected parts, mold changes, electrical failures, or shortened product life.
PA66 is often selected for general mechanical strength and cost efficiency. PBT is commonly chosen when low moisture uptake, stable insulation, and balanced dimensional performance are more important. LCP becomes attractive when the component has very thin walls, fine pitch terminals, high temperature exposure, or demanding flow requirements.
However, no material is automatically superior in every application. Glass fiber content, flame-retardant additives, mineral fillers, impact modifiers, colorants, mold design, insert geometry, and processing conditions can change the final result significantly.
The following values are general engineering ranges. Exact performance depends on the specific grade, reinforcement level, flame-retardant package, test method, and processing history. The selected supplier should confirm the final datasheet and regulatory status before production approval.
| Parameter | PA66 | PBT | LCP | Why it matters in insert molding |
|---|---|---|---|---|
| Typical melt processing range | 260 to 300 C | 230 to 270 C | 300 to 360 C | Controls mold temperature, insert protection, cycle time, and degradation risk |
| Glass transition temperature | Approximately 45 to 55 C | Approximately 40 to 60 C | Approximately 100 to 150 C depending on grade | Indicates how the resin responds as temperature rises |
| Melting temperature | Approximately 255 to 265 C | Approximately 220 to 230 C | Approximately 280 to 350 C | Affects processing temperature and heat resistance |
| Moisture absorption at equilibrium | Approximately 2.5 to 3.5 percent | Approximately 0.1 to 0.3 percent | Generally below 0.1 percent | Influences dimensions, insulation, drying requirements, and long-term stability |
| Specific gravity | Approximately 1.13 unfilled | Approximately 1.31 unfilled | Approximately 1.40 to 1.45 unfilled | Influences component weight and material usage |
| Tensile strength | Approximately 70 to 85 MPa unfilled | Approximately 50 to 65 MPa unfilled | Approximately 120 to 180 MPa for many grades | Indicates resistance to mechanical loading and insert retention stress |
| Flexural modulus | Approximately 2.5 to 3.0 GPa unfilled | Approximately 2.3 to 2.8 GPa unfilled | Approximately 4 to 10 GPa depending on reinforcement | Indicates rigidity around terminals and thin walls |
| Continuous-use temperature | Approximately 100 to 120 C | Approximately 120 to 140 C | Approximately 150 to 220 C depending on grade | Helps determine service life near heat-generating electrical parts |
| Dimensional stability in humidity | Low to moderate | Good | Very good | Important for terminal spacing, sealing, and connector fit |
| Thin-wall flow | Moderate | Good | Excellent | Determines whether small cavities and fine features fill completely |
| Typical relative material cost | Low to medium | Medium | High | Must be evaluated against tooling, yield, and field reliability |
A higher tensile strength value does not automatically mean better insert retention. The actual result also depends on the insert surface, undercuts, knurling, shrinkage, wall thickness, gate location, and cooling profile.
Likewise, a lower moisture absorption value does not guarantee better electrical reliability if the design has poor creepage distance, trapped contamination, insufficient venting, or an unsuitable flame-retardant system.
PA66 provides a useful combination of mechanical strength, toughness, wear resistance, and process availability. Glass-fiber-reinforced PA66 is widely considered when an electrical component must withstand assembly force, vibration, clips, brackets, or repeated mechanical loading.
PA66 absorbs considerably more moisture than PBT or LCP. As moisture content changes, the material can change in dimensions, stiffness, impact behavior, and electrical properties. This does not make PA66 unsuitable, but it requires a controlled specification and realistic validation plan.
Drying is especially important before molding. Poorly dried PA66 may produce surface defects, reduced molecular weight, weak weld lines, or inconsistent mechanical performance. Storage conditions after drying also matter because the resin can reabsorb moisture before processing.
PA66 is often suitable for purchasing groups that prioritize mechanical durability, established processing capability, and moderate material cost. It is a strong candidate when the product operates in a controlled environment and the design can tolerate some moisture-related dimensional change.
For example, PA66 can work well in an insert-molded bracket with embedded threaded metal parts, a cable retention component, or a sensor housing where mechanical loading is more severe than precision electrical spacing.
PBT is frequently selected for electrical connectors, terminal housings, relay parts, coil formers, sensor bodies, and switch components. Its low moisture absorption helps maintain more consistent dimensions and insulation behavior than many polyamide grades.
When the application requires reliable insulation and stable geometry but does not require the extreme thin-wall flow or temperature capability of LCP, PBT often provides the most balanced solution.
PBT generally absorbs less moisture than PA66, so the terminal position and connector fit are less sensitive to humidity. This can simplify dimensional validation and reduce the risk of field changes in contact spacing.
PBT is often appropriate for purchasing groups seeking a dependable balance between performance and cost. It is especially attractive when the component must maintain electrical spacing and dimensional accuracy through humidity exposure, but the mold does not require the extreme flow capability of LCP.
Typical applications include connector bodies, relay bases, terminal blocks, coil bobbins, sensor housings, switch components, and insert-molded parts used in automotive or industrial control systems.
LCP has a highly oriented molecular structure that provides excellent flow into narrow cavities. This makes it useful for fine-pitch connectors, miniature switches, high-density terminal components, bobbins, sockets, and components with long flow lengths relative to wall thickness.
LCP is not simply a premium substitute for PA66 or PBT. Its high melt temperature places greater demands on the injection unit, mold design, hot runner system, insert material, and process controls.
The material can also show strong anisotropy because of molecular and filler orientation. A part may be very stiff in one direction and less robust in another. Weld lines, gate location, flash control, venting, and insert positioning must therefore be evaluated during mold-flow and prototype development.
LCP is most suitable for purchasing groups whose products have strict dimensional tolerances, very thin walls, high pin density, high operating temperature, or limited cavity space. The higher material cost can be justified when it prevents incomplete filling, excessive warpage, additional assembly steps, or field failures.
Typical applications include miniature connectors, high-density terminal carriers, coil formers, sensor components, camera and optical modules, high-temperature control parts, and compact battery or power electronics components.
PA66, PBT, and LCP do not usually determine battery life directly in the way that a battery cell, motor, or power-management circuit does. Their influence is indirect but still important.
For a compact battery-powered device, LCP may enable thinner walls and smaller connector geometry. PBT may provide stable insulation and dimensions at a lower cost. PA66 may be adequate when the component is mainly structural and the environment is not highly humid or temperature-intensive.
Products used in vehicles, outdoor equipment, industrial controls, and battery systems can experience repeated temperature changes. PBT and LCP generally offer more stable dimensions than moisture-sensitive PA66, especially when the component includes closely spaced terminals or mating connector features.
PA66 can still perform well when the material is conditioned correctly and the design accounts for moisture-related movement. The key is to validate the part at dry, conditioned, hot, cold, and humid states rather than testing only a new molded sample.
Metal insert retention is influenced by the thermal shrinkage of the polymer, the insert geometry, the surface texture, the resin flow, and the stress created during cooling. A resin with high strength may still fail if the insert is poorly supported or if the plastic wall is too thin.
Short-term dielectric testing on dry samples may not represent field performance. The validation plan should include humidity conditioning, high-temperature exposure, thermal cycling, voltage stress, vibration, and chemical contact when applicable.
PBT and LCP generally offer an advantage where moisture-driven changes in insulation or dimensions are a major concern. PA66 requires a more deliberate conditioning strategy, but it can still meet electrical requirements when the selected grade and design are properly controlled.
PA66 is widely available and familiar to many molding suppliers. This can reduce material procurement risk and simplify supplier qualification. However, drying, moisture control, warpage, and conditioning should be included in the production cost calculation.
PBT typically costs more than standard PA66 but may reduce the need for extensive moisture compensation. Its dimensional stability can lower assembly problems in connectors and terminal parts. The final cost advantage depends on volume, geometry, testing requirements, and the consequences of a field failure.
LCP has the highest resin cost in this comparison, but it may reduce total system cost when it eliminates secondary assembly, enables a smaller component, improves cavity filling, or supports a higher-temperature design.
Material selection and Insert Overmolding Services should be evaluated together. A resin that performs well in a laboratory may not be the best choice if the supplier cannot control drying, insert placement, mold temperature, cavity balance, or inspection.
Resin datasheets are useful for screening, but the insert-molded component is the real product. The metal insert, molded geometry, gate location, weld lines, surface condition, and cooling history can change the performance significantly.
Testing should reflect how the component will actually be used. A battery module connector may require vibration, humidity, thermal cycling, and insulation testing. A miniature sensor may require fine dimensional control and chemical resistance. A relay base may require repeated thermal exposure and flame-retardant performance.
Testing only dry, room-temperature samples can make PA66 appear more stable than it will be in a humid environment. Testing only one short molding run can hide LCP orientation problems or PBT hydrolysis-related degradation. A production-intent validation plan gives the purchasing group a more reliable basis for supplier and material approval.
PA66 is a practical choice for strong, cost-sensitive components. PBT is often the most balanced option for electrical insulation and dimensional stability. LCP is the specialist option for thin-wall, high-temperature, and high-precision designs.
The final choice should consider:
Onlink can support the material selection process by connecting resin choice with insert design, mold construction, process control, and production validation. Instead of selecting PA66, PBT, or LCP from a single datasheet value, the purchasing group can evaluate the complete insert-molded assembly and its expected service conditions.
For a cost-sensitive structural part, PA66 may provide the right balance. For a stable electrical housing, PBT may offer the most practical solution. For miniature, thin-wall, or high-temperature components, LCP may justify its premium cost. A controlled design review, prototype run, and production-intent test plan can turn that comparison into a reliable purchasing decision.


