Sep.08,2026
For buyers comparing stamped motor laminations for mass production with laser-cut motor laminations for prototypes, the decision affects unit cost, magnetic performance, tooling investment, and delivery risk. A qualified Electric Motor Core Parts Manufacturer will evaluate the stator core, rotor core, and electrical steel grade together rather than judging the process by price alone. In practical terms, lamination factor, burr height, and core loss often determine whether a motor reaches its efficiency target after thousands of operating hours.
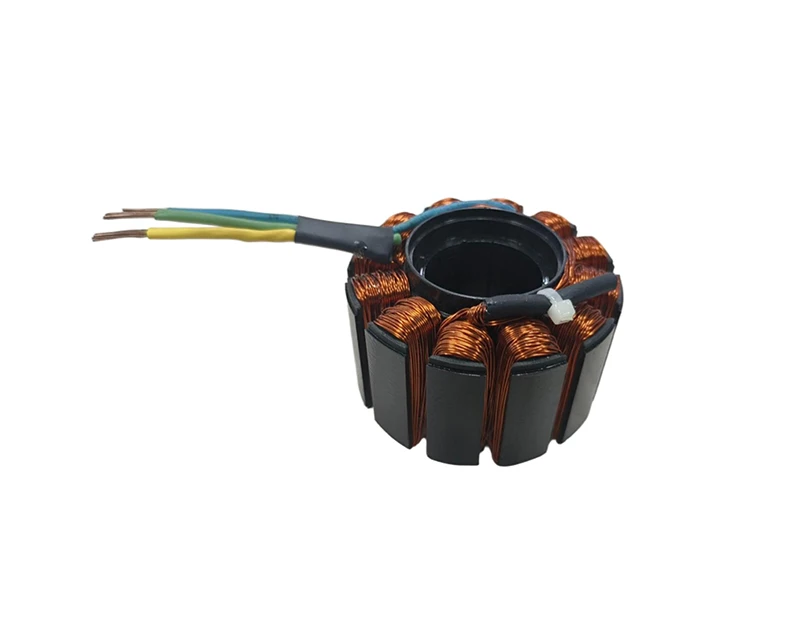
The question usually appears after a design team receives two quotations: one with a large progressive-die charge and another with a higher per-piece price but no tooling fee. A prototype may look identical under a caliper, yet its production behavior can differ substantially. The correct choice depends on annual volume, material thickness, geometry, tolerance requirements, motor speed, noise targets, and how quickly the design may change.
Both processes produce individual laminations from electrical steel, usually non-oriented silicon steel for general-purpose motors or specialized grades for high-efficiency and high-speed applications. The laminations are then stacked, bonded, welded, riveted, or interlocked to form the stator and rotor core.
Stamping uses a punch and die. In high-volume production, a progressive die can perform piercing, slotting, indexing, and cut-off operations in one continuous press cycle. Laser cutting uses a focused beam to cut the profile directly from a sheet or stack. It does not require a dedicated progressive die, which makes it attractive when the design is still changing.
That difference creates a clear commercial trade-off:
For a 50 mm to 150 mm motor lamination, the process may also influence the heat-affected zone, edge burrs, residual stress, dimensional stability, and local magnetic properties. These effects are manageable, but they must be included in the engineering review instead of treated as secondary details.
A progressive stamping line feeds electrical steel strip through a sequence of stations. Pilot holes maintain registration, while punches create the shaft bore, ventilation openings, slots, and outer profile. The finished laminations may be automatically stacked and interlocked during the same operation.
For mature designs, this process can achieve production rates from several hundred to more than 1,000 strokes per minute, depending on lamination size, material thickness, press capacity, and the number of parts produced per stroke. A carefully maintained die can hold many critical dimensions within approximately ±0.02 mm to ±0.05 mm, although the actual result depends on the geometry and inspection method.
Stamping is particularly effective when:
The main technical risk is not the cutting speed. It is progressive die condition. A worn punch can increase burr height, distort slot geometry, and produce inconsistent stacking pressure. For many motor programs, a burr target below 0.03 mm to 0.05 mm is used as a practical control point, but the acceptable value must be confirmed against insulation coating, stack height, and short-circuit risk.
The strongest advantage is cost behavior. Once the die is qualified, the material and press time dominate the unit cost. A production line can therefore deliver a much lower price per lamination than laser cutting.
Stamping also supports automated interlocking. Small tabs can be formed into each lamination so the stack holds together without a separate adhesive operation. This reduces handling and can improve takt time. However, interlocking changes the local magnetic path and may increase loss if the design uses too many tabs or places them in high-flux regions.
Tooling is the limitation. A progressive die for a motor core may cost from several thousand dollars to more than $100,000, depending on size, station count, steel grade, precision, and automation. The die also requires engineering approval, trial runs, correction cycles, spare components, and preventive maintenance.
Stamping is therefore not automatically economical at low volume. If a customer orders only 5,000 sets, a tooling charge can make the first production batch more expensive than laser-cut parts even when the stamped unit price is lower.
Laser cutting starts with a CAD profile. The beam follows the programmed contour, allowing a supplier to produce a new design without manufacturing a dedicated die. This is valuable for startup motors, research programs, small industrial drives, and motors undergoing electromagnetic optimization.
A laser-cut batch can normally be prepared in days rather than the several weeks or months often required for a new progressive die. The exact schedule depends on nesting, material availability, programming, inspection, and stack assembly. For early prototypes, this shorter path can prevent a tooling investment before the motor has passed thermal, acoustic, and load testing.
Laser cutting is useful when the design includes:
The process can produce fine features, but “laser precision” should not be treated as a guarantee of perfect magnetic performance. Cutting speed, power, focus, assist gas, material grade, and sheet thickness affect the edge. A heat-affected zone can create localized residual stress and alter permeability near the cut edge. For a high-performance motor, the manufacturer may need to evaluate the cut-edge condition through magnetic testing, dimensional inspection, and loss measurement.
The largest disadvantage is throughput. A laser must trace the profile, so the cutting time increases with perimeter length and feature count. A complex 100 mm lamination may require seconds or longer per piece, while a stamping press can produce several parts per second after setup.
Laser cutting can also leave dross or a heat-affected edge if the parameters are poorly controlled. In many applications, the resulting burr or edge condition remains acceptable, but the customer should specify maximum burr height, edge roughness, dimensional tolerance, and magnetic validation requirements in the drawing.
Another issue is stack consistency. Laser-cut laminations are commonly stacked manually or with a separate fixture. That can increase labor time and variation in stack height. Bonding, welding, or mechanical compression may be required to achieve the target axial length and rigidity.
| Parameter | Progressive Stamping | Laser Cutting | Production Meaning |
|---|---|---|---|
| Tooling investment | Approximately $5,000–$100,000+, depending on die complexity | Usually no dedicated die; programming and fixtures are required | Laser reduces initial commitment; stamping lowers long-run unit cost |
| Typical economic volume | Often above 50,000–100,000 motor sets | Often below 10,000–30,000 motor sets | Break-even depends on tooling amortization and geometry |
| Cycle speed | Hundreds to more than 1,000 strokes per minute in suitable applications | Usually seconds or longer per lamination, depending on perimeter | Stamping is better for automated high-volume production |
| Design change flexibility | Low after die completion; changes may require die modification | High; CAD changes can be programmed without a new die | Laser cutting reduces development risk |
| Dimensional repeatability | Strong after die qualification; commonly controlled in the hundredths of a millimeter | Good, but affected by thermal distortion and parameter control | Both can meet demanding requirements with process validation |
| Edge condition | Burr from punch clearance and tool wear | Heat-affected zone, dross, and possible taper | Edge inspection is essential for both methods |
| Stacking method | Interlocking or automated stacking is readily available | Often requires fixtures, bonding, welding, or manual stacking | Stamping generally simplifies high-volume assembly |
| Material utilization | Efficient strip nesting after die layout optimization | Flexible nesting, but scrap depends on sheet layout and part shape | Material utilization affects total cost more than cutting price alone |
| Magnetic impact | Plastic deformation and burr stress near punched edges | Thermal stress near laser-cut edges | Core loss and permeability should be tested, not assumed |
Electrical steel laminations reduce eddy-current loss by interrupting the conductive path through the core. The final motor performance depends on steel grade, lamination thickness, coating integrity, stacking factor, stress state, and operating frequency.
A common stacking factor for insulated electrical steel may fall around 0.93 to 0.98, depending on coating, flatness, pressure, burrs, and the stacking method. If a design requires a 50 mm magnetic stack and the effective stacking factor is 0.95, the physical stack may need to be approximately 52.6 mm before compression and dimensional correction.
Punching can introduce plastic deformation around the edge. Laser cutting can introduce thermal stress. Both effects may increase local iron loss. In a motor operating at high electrical frequency, even a small increase in core loss can affect winding temperature and efficiency. For that reason, a serious supplier should review:
For example, if a 1.5 kW induction motor loses an additional 20 W in the core because of poor edge control or excessive magnetic stress, that heat must be removed through the housing. A motor originally designed for a 90°C temperature rise may no longer meet the thermal margin under the same load.
Consider a customer producing 250,000 motor sets per year with one fixed stator and rotor design. The progressive die costs $60,000, while the stamped lamination cost is estimated at $0.18 per set-equivalent. Laser cutting costs $1.20 per set-equivalent because of machine time and labor.
The approximate first-year cost comparison is:
In this simplified case, stamping saves about $195,000 in the first year. If the design remains unchanged, the difference becomes larger in later years because the die cost has already been absorbed. Stamping is the practical choice, provided the supplier can maintain die condition, material availability, and inspection control.
Now consider an engineering team developing a 20,000 rpm permanent-magnet motor. The rotor has flux barriers that may change after electromagnetic simulation and overspeed testing. A $45,000 die would create financial exposure before the rotor design is stable.
Laser cutting may cost more per piece, but a 500-set prototype batch can be produced without locking the geometry. The team can compare air-gap flux density, vibration, back EMF, temperature rise, and rotor balance before approving production tooling. In this situation, the flexibility of laser cutting has measurable engineering value, even if the prototype unit price is five or six times higher than the eventual stamped price.
A specialized pump manufacturer may need 15,000 motor sets annually, with three similar stator designs and frequent slot changes. The correct answer may not be a simple “stamp or laser” decision. Laser cutting can support the first 3,000 to 10,000 sets while the customer confirms demand. If the annual volume later rises above 80,000 sets, the supplier can transfer the validated geometry to a progressive die.
This staged approach avoids premature tooling while preserving a path to lower unit cost. It also allows the customer to use prototype and pilot production data to optimize slot fill, noise, winding insertion, and stack height before mass production.
The basic break-even quantity can be estimated with this formula:
Break-even quantity = (Stamping tooling cost − Laser setup cost) ÷ (Laser unit cost − Stamped unit cost)
Suppose the die costs $30,000, laser setup costs $2,000, laser cutting costs $0.90 per lamination set, and stamping costs $0.25 per set. The calculation is:
($30,000 − $2,000) ÷ ($0.90 − $0.25) = approximately 43,077 sets.
At volumes above roughly 43,000 sets, stamping may have the lower direct manufacturing cost. This estimate excludes inventory, maintenance, die repair, scrap, freight, inspection, and the cost of changing the design. If the design is likely to change before 43,000 sets are consumed, laser cutting may still provide the lower total project cost.
Material utilization deserves separate attention. A supplier that reduces steel scrap from 25% to 18% can offset part of the cutting-price difference, especially when electrical steel prices are high. Buyers should request a quotation that identifies material grade, thickness, utilization assumptions, stacking method, tooling amortization, and expected scrap rate.
One documented development pattern seen by motor manufacturers follows a practical two-stage route. An engineering customer began with laser-cut stator and rotor laminations because the slot opening and rotor bridge were still being revised. The first batch was used for winding trials, no-load testing, load testing, and acoustic evaluation.
During testing, the team changed the rotor bridge dimension and adjusted the stator tooth tip. Because no new die was required, the updated prototype was produced without restarting the tooling process. After the electromagnetic and mechanical design was frozen, the customer moved to progressive stamping for the larger production quantity.
The important result was not simply a lower piece price. The team avoided paying for a die that would have required modification after the first test cycle. Once the design stabilized, stamping improved production rhythm, automated stacking, and batch-to-batch consistency. This case illustrates why laser cutting and stamping are often sequential technologies rather than competing technologies.
In another production review, a customer initially selected the lowest laser-cut quotation but later experienced inconsistent stack height because manual stacking pressure was not specified. The supplier corrected the issue by defining the lamination count, compression force, bonding method, and final core height tolerance. The lesson is direct: a cutting method cannot compensate for an incomplete core assembly specification.
Feedback from motor purchasers and production engineers tends to focus on four practical points:
Onlink can be considered when a project requires both prototype flexibility and a defined path toward stamped mass production. The useful question for a supplier is not “Can you cut the lamination?” but “Can you validate the electrical steel, edge condition, stack assembly, and production transfer under the same quality plan?”
Stamping ranks first when annual demand is high, the geometry is frozen, and automated assembly is important. It normally provides the best unit economics, the shortest takt time, and strong repeatability after tooling qualification.
Laser cutting ranks first for new motor programs, low-volume orders, complex geometries, and designs that may change after testing. Its higher unit cost can be justified by reduced tooling risk and faster iteration.
For uncertain demand, begin with laser-cut laminations, complete engineering validation, and transfer to progressive stamping after the design reaches a defined annual volume. This strategy often balances time-to-market and long-term cost.
Do not compare only the price per lamination. Include die cost, expected tool life, scrap, inspection, stacking labor, coating damage, delivery frequency, engineering changes, and the cost of a rejected core stack. A supplier such as Onlink becomes more valuable when it can manage the complete transition from sampling to stable production rather than supplying an isolated cutting operation.
A precise RFQ helps prevent misleading price comparisons. Include the following information:
Ask the manufacturer to provide both a prototype route and a mass-production route. This makes it easier to see whether the supplier has a realistic scale-up plan or is simply quoting the cheapest immediate process.
Stamped motor laminations are suitable for:
Stamped motor laminations may not be suitable for:
Laser-cut motor laminations are suitable for:
Laser-cut motor laminations may not be suitable for:
There is no universal winner. Stamping is normally better for mass production because it combines high throughput, automated stacking, and lower recurring cost after tooling is amortized. Laser cutting is normally better for prototypes, low-volume orders, and designs that are not yet stable.
The most reliable decision is based on break-even quantity, design maturity, core-loss requirements, burr control, stacking method, and the cost of engineering changes. For many motor programs, the strongest route is laser-cut prototypes followed by stamped production laminations after validation.
If you are comparing stamped motor laminations for mass production, laser-cut motor laminations for prototypes, or an electric motor core parts manufacturer for a staged supply plan, ask Onlink for a process comparison based on your annual volume and drawing. Confirm the lamination factor, burr height, and core loss targets before approving the quotation, then select the process that minimizes total production risk rather than only the first invoice.


